
Industrial coating requirements are often ongoing rather than one-time purchases. Manufacturing units, engineering companies, fabrication businesses, and maintenance teams require reliable access to paints, primers, thinners, and protective coating systems that match their operational needs. Selecting the right Industrial Paint Supplier becomes important because coating quality directly affects surface protection, maintenance cycles, and project outcomes.
In Mumbai, where industries operate across sectors such as engineering, fabrication, infrastructure, and manufacturing, businesses need coating suppliers who understand different application requirements and environmental challenges.
Understanding The Role Of An Industrial Paint Supplier
An industrial paint supplier provides access to coating products required for protecting and finishing industrial surfaces. However, a dependable supplier does more than deliver products.
A suitable supplier helps businesses evaluate:
Application requirements
Surface conditions
Environmental exposure
Required coating performance
Product compatibility
Industrial painting involves multiple factors, and selecting the wrong product can lead to premature coating failure.
Evaluate The Product Portfolio
A strong industrial coating supplier should offer solutions across different application categories.
Depending on requirements, industries may need:
P.U. Aliphatic coatings
P.U. Aromatic coatings
P.U. Clear Lacquer
P.U. Primer
Epoxy paints
Epoxy primers
Zinc phosphate primers
High-temperature paints
Synthetic paints
Quick-drying paints
Industrial thinners
A broad product range allows businesses to select coatings according to actual operating conditions.
Consider Application Knowledge
Industrial coatings perform best when selected according to the working environment.
A supplier should understand factors such as:
Corrosion Exposure
Metal surfaces exposed to humidity or coastal conditions may require protective systems designed to reduce corrosion risks.
Temperature Conditions
Equipment operating at high temperatures may require specialised coatings such as H.R. Paint @250°C, H.R. Paint @450°C, or H.R. Paint @600°C.
Chemical Exposure
Industries dealing with chemicals, solvents, or processing materials may require epoxy-based protective solutions.
Importance Of Product Compatibility
Industrial coating systems often include multiple layers. The primer, intermediate coat, final paint, and thinner should work together properly.
For example:
PU coatings require suitable polyurethane-compatible materials
Epoxy systems require appropriate epoxy products and thinners
High-temperature coatings require compatible application materials
Using mismatched products may affect drying, adhesion, and final performance.
Check Support For Different Industrial Applications
A good supplier should understand where products are commonly used.
Industrial coating applications may include:
Machinery protection
Fabricated structures
Equipment finishing
Steel components
Storage systems
Maintenance projects
The supplier’s ability to recommend suitable options based on application requirements can simplify the selection process.
Avoid Common Supplier Selection Mistakes
Businesses often make mistakes by focusing only on product price.
Important factors to consider include:
Product suitability
Consistency
Technical understanding
Availability
Long-term reliability
A lower-cost coating that fails early may increase maintenance expenses over time.
Industrial Coating Support For Mumbai Businesses
Mumbai’s industrial environment creates unique coating challenges due to humidity, coastal exposure, and varied operational conditions. Businesses require protective coating solutions that support durability and efficient maintenance planning.
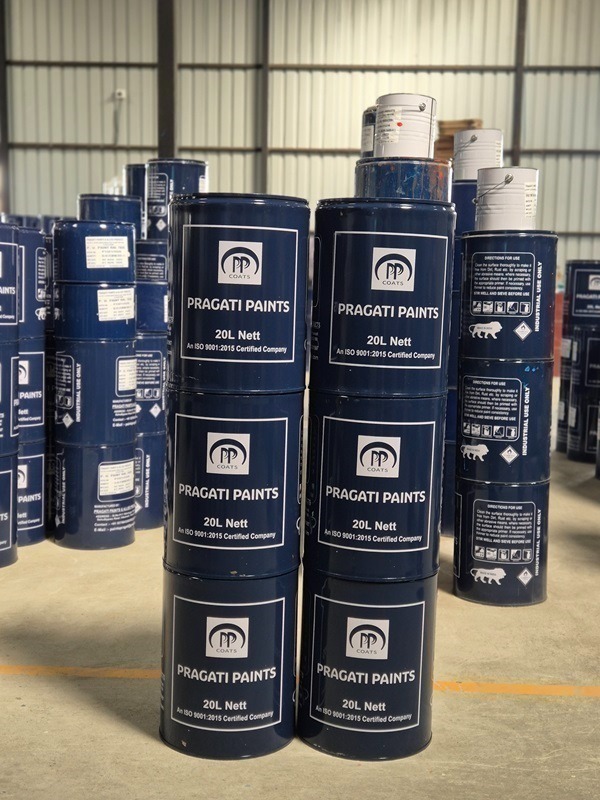
Pragati Paints and Allied Products provides industrial coating products for different requirements, including polyurethane, epoxy, high-temperature, and protective coating systems.
Selecting the right industrial paint supplier involves understanding product capability, technical requirements, and application conditions. A reliable supplier relationship helps industries maintain better coating performance and manage future requirements more effectively.